Buy more, save more
- 3–5 rolls 3% off
- 6–9 rolls 6% off
- 10–19 rolls 10% off
- 20+ rolls 15% off
Discount is applied automatically in your cart.
Matte PETG
$17.95
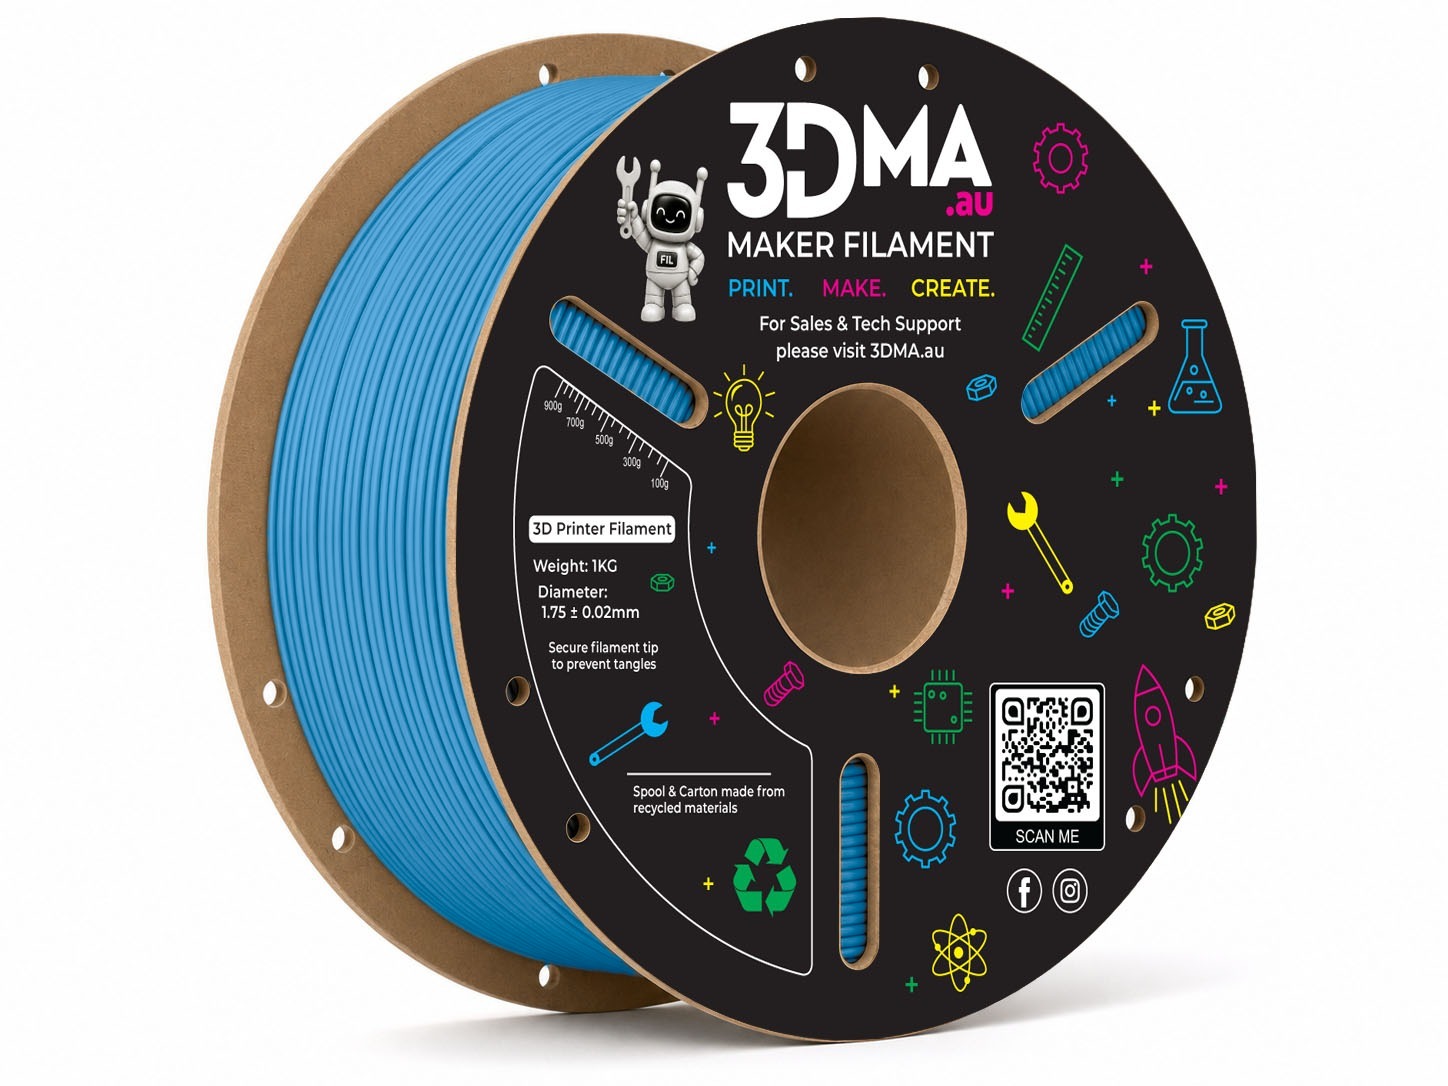
1.75 mm diameter · 1 kg net filament per spool
Matte PETG gives us the strength and everyday durability of PETG with a smooth, glare-free matte surface that hides layer lines and resists fingerprints — ideal for enclosures, display pieces and functional parts you actually look at.
Printing & drying
- Material
- PETG
- Diameter
- 1.75 mm
- Spool
- 1 kg net
- Nozzle
- 230–250°C
- Bed
- 45–60°C
- Printing speed
- 40–100 mm/s
- Part cooling
- Low to medium
- Enclosure
- Not required
- Nozzle type
- Standard brass
- Drying
- 60 ± 5°C for 12h
These are typical working ranges for orientation. The label on the spool you receive is authoritative for that batch. More detail in the storage and drying guide and the troubleshooting guide.
Shipping
- Packed and dispatched from Sydney, Australia.
- Every spool ships sealed with desiccant.
- Tracking is provided on every order.
- Buying more than a few spools? Bulk Orders gets you a quote and a supply plan.
Current delivery timeframes are on the Shipping & Returns page.
Returns & warranty
- Backed by the Australian Consumer Law.
- Spool faults are a product fault, not a settings problem. Contact us with your order number and photos.
- Not sure whether it is the spool or the printer? The five-minute triage tells you which half is at fault.
Full terms on the Shipping & Returns page.
Material details
Matte PETG is the one to reach for when the part will be looked at as well as used. It keeps the water resistance, chemical tolerance and everyday durability that make PETG the sensible default for functional printing, then trades the glossy surface for a soft, even matte that swallows layer lines, kills glare and barely shows a fingerprint. If you have ever printed something that worked perfectly and still looked like a 3D print, this is the fix.
What Matte PETG is good for
The matte effect comes from filler particles that scatter light instead of reflecting it. That changes more than the look: it diffuses the tiny ridges between layers, so the same model printed in Matte PETG reads as moulded rather than printed. It also changes the mechanical profile, which is why this is a different material from our standard PETG rather than the same thing in a different finish.
How Matte PETG prints
The published window is a nozzle at 230–250 °C and a bed at 45–60 °C with adhesive, at 40–100 mm/s with the cooling fan on. Three of those numbers deserve a second look, because they are not what PETG printers expect.
The bed runs cool. Most PETG asks for 70–85 °C. Matte PETG wants 45–60 °C. If you load it into an existing PETG profile without changing the bed, you will get elephant-foot on the first layers and a part that fuses itself to the plate. Drop the bed first.
The fan stays on. Glossy PETG is usually printed with minimal cooling to protect layer bonding. The filler in Matte PETG changes how it sets, and the manufacturer specifies the fan on. Leave it on.
It is not a speed material. The ceiling is 100 mm/s, against up to 600 mm/s for Ultra PETG High Flow. Filled filaments need time for the melt to flow evenly, and pushing past the window shows up as patchy sheen where the matte goes inconsistent. If you want tough PETG parts in a hurry, print the high-flow grade and accept the gloss.
Maximum unsupported overhang is 55°, a little tighter than plain PETG, so add supports slightly earlier than you would otherwise. Retraction sits at 20–40 mm/s. Bed adhesive is worth using: a cool bed plus a matte surface is a less grippy combination than glossy PETG on a hot plate.
What Matte PETG will not do
It will not take heat. Heat deflection is 51 °C. That is well under standard PETG at 72 °C, and under Core PLA at 57 °C. A part left on a dashboard through an Australian summer will deform. For anything warm, use Ultra PETG High Flow, and for genuine heat use Ultra ABS High Flow or Core ASA.
It is not the stiffest option. Bending modulus is 1119 MPa, roughly half that of our standard PETG. In practice the part flexes further under the same load. For a clip or a hinge that is a feature; for a long bracket that should not sag, it is not.
Impact resistance is mid-range. At 33 kJ/m² it takes a knock better than PLA and less well than standard PETG. Tensile strength, interestingly, is higher at 49.8 MPa, and elongation at break reaches 56%, so it stretches a long way before it finally lets go rather than cracking suddenly.
It will not survive full sun indefinitely. Like all PETG it is fine under an eave or in a shed, but for parts in direct Australian UV, Core ASA is the right material.
Every colour, one material
Matte PETG comes in nine colours — black, white, grey, blue, green, red, orange, pink and yellow — and every one is the same base polymer with the same print settings. Change colour mid-project without touching your profile. Matte finishes read deeper and more saturated than gloss in photographs, and the darker colours in particular lose the plastic look entirely. Browse the full palette on the colours page.
Printer compatibility
Any modern FDM printer running 1.75 mm filament will handle it. No enclosure is needed. A brass nozzle is fine — the matting filler is not abrasive in the way carbon or glass fibre is, so you do not need a hardened nozzle. Direct drive and Bowden both work. If your printer already prints PETG, it will print this, provided you drop the bed temperature and turn the fan on.
Spools are 1 kg with roughly 330 m of filament, at a diameter tolerance of ±0.02 mm.
Storage, drying and shelf life
PETG absorbs moisture from the air, and Matte PETG is thirstier than most — saturated water absorption is 0.40%. Wet filament prints with stringing, surface bubbles and a blotchy finish that defeats the point of buying a matte material in the first place.
Dry it for 12 hours at 60 ± 5 °C before printing. That is longer than the 8 hours most PETG asks for, and it is the single most common cause of disappointing matte prints. Store the spool sealed with desiccant at 20% relative humidity or lower between sessions. Unopened and sealed, it keeps indefinitely; opened and left on the shelf in a humid Sydney summer, it can need drying again within a fortnight.
Common questions about Matte PETG
What is the difference between Matte PETG and normal PETG?
Finish and mechanical profile. Matte PETG has filler that scatters light, so it hides layer lines and glare. It is also more ductile, less stiff, slower to print and considerably less heat resistant — 51 °C against 72 °C. Choose matte when the part is seen, and standard PETG when it works hard or gets warm.
Why do my matte prints look patchy?
Almost always moisture, or speed. Dry the spool for 12 hours and keep the nozzle inside 230–250 °C at no more than 100 mm/s. Uneven sheen is the filler failing to distribute evenly, which is what happens when the melt is pushed too fast or is carrying water.
Do I need to change my PETG profile?
Yes, in two places. Drop the bed to 45–60 °C, and turn the cooling fan on. Leaving a standard PETG profile in place is the most common reason a first print goes wrong.
Does Matte PETG need a hardened nozzle?
No. The matting agent is not abrasive like carbon fibre or glass fibre. A standard brass nozzle is fine for the life of the spool.
Can I sand or paint it?
Yes, and it takes paint better than glossy PETG because the surface already has tooth. Light sanding will polish the matte away in patches, so if you are painting, prime rather than sand where you can.
Is it food safe?
No printed part should be treated as food safe. Layer lines harbour bacteria regardless of the polymer, and neither the base material nor the colourants are certified for food contact in printed form.
How much can I print from a 1 kg spool?
Roughly 330 m of 1.75 mm filament. For typical 0.2 mm layers at 15% infill that is somewhere between 25 and 40 medium models, though geometry and wall count move that number a lot.
Which should I pick, Matte PETG or Matte PLA?
Matte PLA is easier to print, holds finer detail and is the better choice for a display model that never leaves a desk. Matte PETG is tougher, bends instead of snapping and shrugs off water, so it is the one for a part that gets handled or lives somewhere damp. Neither likes heat — if the part gets warm, both are the wrong answer.
Still not sure?
The materials guide compares every material in the range side by side, and if a part faces several problems at once, ask us — material recommendations are free and we enjoy giving them.
Technical specifications
Preparation Before Printing
- Drying settings (blast drying oven)
- 60 ± 5 °C for 12h
- Printing & storage humidity
- ≤ 20% RH (Sealed with Desiccant)
Recommended Printing Settings
- Nozzle temperature
- 230 - 250 °C
- Bed temperature (with glue)
- 45 - 60 °C
- Printing speed
- 40 - 100 mm/s
- Retraction speed
- 20 - 40 mm/s
- Cooling fan
- On
- Max overhang angle
- 55°
Physical Properties
- Density
- 1.35 g/cm³
- Saturated water absorption (25 °C, 55% RH)
- 0.40%
- Heat deflection temperature
- 51 °C
Mechanical Properties
- Tensile strength
- 49.79 MPa
- Elongation at break
- 56.1%
- Bending strength
- 41.21 MPa
- Bending modulus
- 1119.41 MPa
- Impact strength
- 33.15 kJ/m²
Manufacturer figures for PETG Matte, from PETG Matte Technical Data Sheet V1.0. Test values are measured on standard samples and are for design comparison — real-world results depend on your printer, settings and model.
Reviews
There are no reviews yet.